

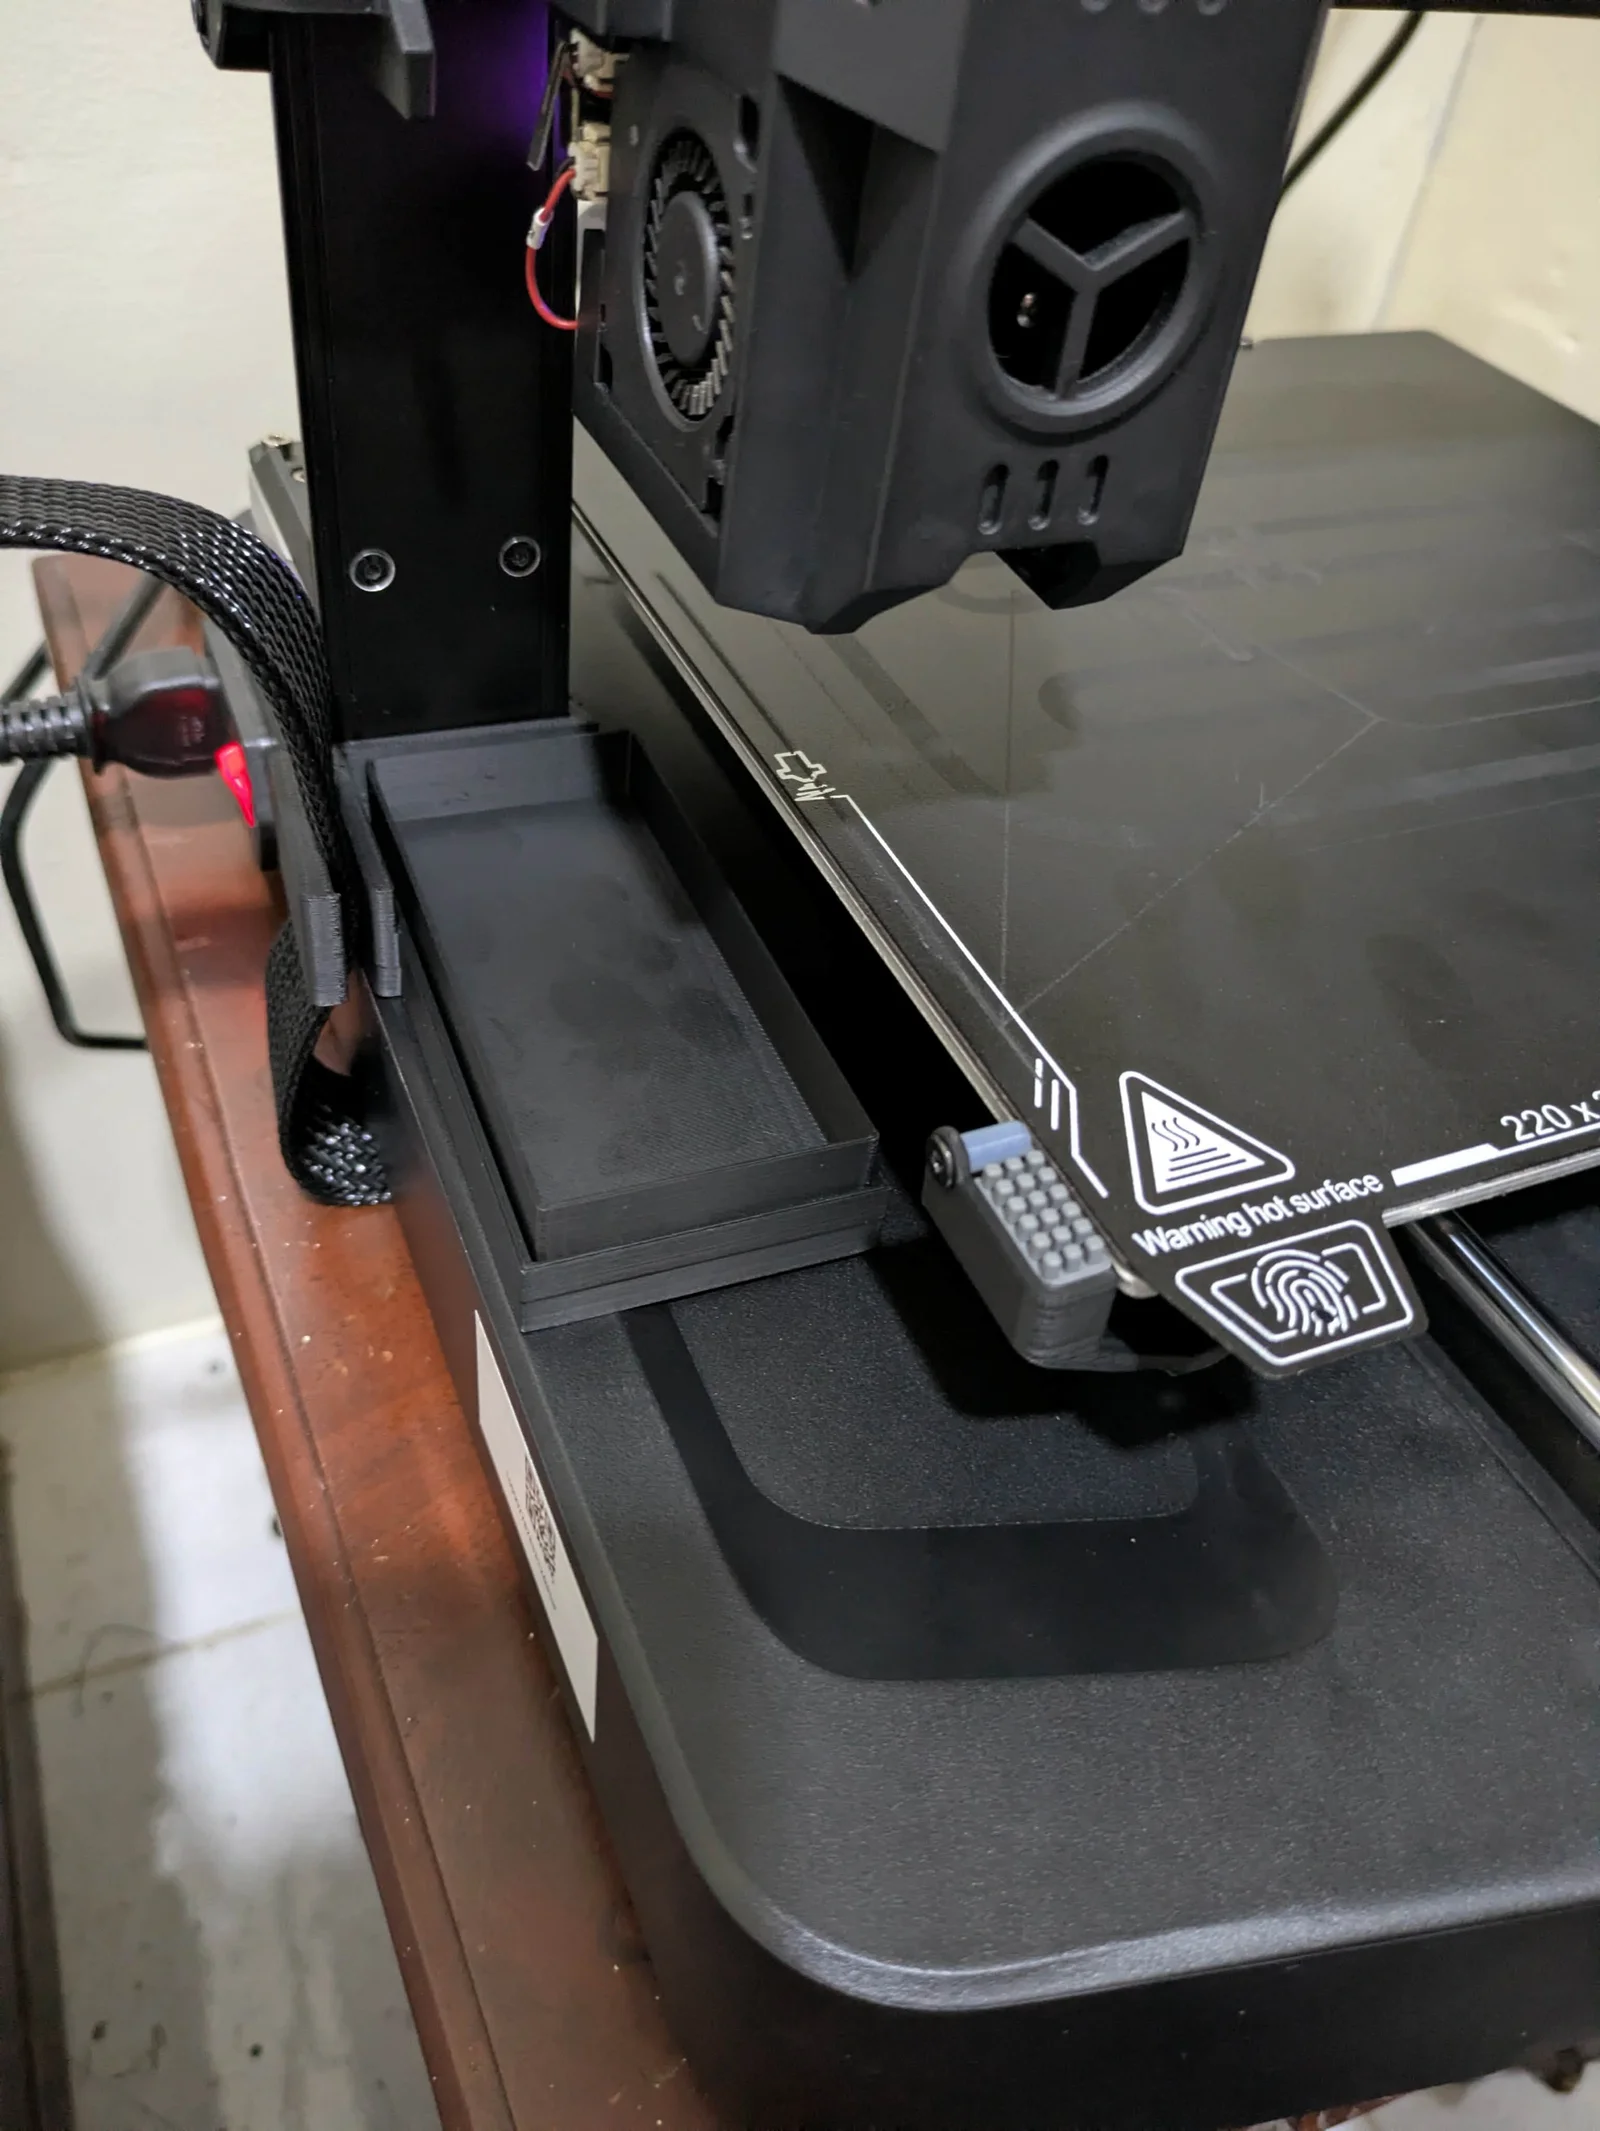

Kẹp giữ sợi Filament
 Bytinx_1344834Likes1.2KDownloads6K
Remix of Khay Tháo Rời & Giá Đỡ Dây Cáp + Nắp Cho Ender 3 v3 KE / SE By fonzy_815871
Build another version of this model.
1x M3 6mm (I used a thin flat head)
~8mm PTFE tube
A1 Silicon Brush (cut to 16mm or 6 studs)
M4 nut (i used a square nut)
Cut the silicon brush down to 16mm or 6 studs and stick it as shown on the images
Screw in the PTFE tube make sure it is flush with the silicon brush
Mount the wiper to the lower left corner and secure it using the M4 nut.
Mount the bucket holder to the left side gantry and attach the cable
; === Safe Start G-code with Purge + Relative Flicker + Z lift + Purge Line ===
M220 S100 ; Reset Feedrate
M221 S100 ; Reset Flowrate
; Heat bed
M140 S[bed_temperature_initial_layer_single] ; Set bed temp (no wait)
M104 S0 ; Keep nozzle cold
; Home axes
G28
; Full bed leveling
G29
; Move to purge start position safely
G0 Z10 F5000 ; Raise nozzle to safe height
G0 X-10.7 Y25 F6000 ; Move to purge XY position at Z=10
G0 Z+3 F5000 ; Lower nozzle to starting purge height
; Wait for bed temp, then heat nozzle
M190 S[bed_temperature_initial_layer_single] ; Wait for bed temp
M104 S[nozzle_temperature_initial_layer] ; Start nozzle heating
M109 S[nozzle_temperature_initial_layer] ; Wait for nozzle to reach temp
; Purge filament
G92 E0 ; Reset extruder
G1 E25 F300 ; Extrude 25mm slowly
M400
; Blast blower fans for 10s
M106 P0 S255
G4 P20000
M106 P0 S0
; Move back to Y = 18 after purge
G0 Y18 Z-1 F6000 ; Move nozzle to Y=18 at moderate speed
; Relative mode for flicker/wipe
G91
; --- Flicker/wipe sequence (Z from -1 to -1.5, 5 cycles, mm/min) ---
G0 Y-25 F18000
G0 Y25 F18000
G0 Z-0.1 F3000
G0 Y-25 F18000
G0 Y25 F18000
G0 Z-0.1 F3000
G0 Y-25 F18000
G0 Y25 F18000
G0 Z-0.1 F3000
G0 Y-25 F18000
G0 Y25 F18000
G0 Z-0.1 F3000
G0 Y-25 F18000
G0 Y25 F18000
G0 Z-0.1 F3000 ; Final Z reaches -1.5
; Switch back to absolute mode and lift Z safely
G90 ; Absolute positioning
G0 Z10 F1500 ; Lift to safe height at moderate speed
; Purge line routine
G92 E0
G1 X-2.0 Y20 Z0.3 F5000.0 ;Move to start position
G1 Z0.2 ;Lower nozzle to printing height
G1 Y145.0 F1500.0 E15 ;Draw the first line
G1 X-1.7 F5000.0 ;Move to side a little
G1 Y30 F1500.0 E15 ;Draw the second line
G92 E0
G91 ; Relative positionning
G1 E-2 F2700 ; Retract a bit
G1 E-2 Z0.2 F2400 ; Retract and raise Z
G1 X5 Y5 F3000 ; Wipe out
G1 Z5 ; Raise Z more
G90 ; Absolute positionning
G1 X2 Y218 F3000 ; Present print
M106 S0 ; Turn-off fan
M104 S0 ; Turn-off hotend
M140 S0 ; Turn-off bed
M84 X Y E ; Disable all steppers but Z
Bytinx_1344834Likes1.2KDownloads6K

 Byprusa-researchLikes0Downloads2.7K

 ByBrokentooth_designsLikes17Downloads147

 Byarhi_585078Likes64Downloads542

 Bygafyx3dLikes0Downloads121

 ByHanzo3dLikes155Downloads415

 BydarienLikes0Downloads1K

 ByGeek5DLikes147Downloads485

 Byla-cave-au-chatLikes0Downloads965

 Bycrawler-3903250Likes0Downloads906

 ByvertigomakesLikes0Downloads562

 By3DSourcererLikes48Downloads377