


Bear/Bär #4 - Mô hình Gấu WildRock trang trí cực chất
 ByYvaneke589_274368Likes0Downloads5
Build another version of this model.
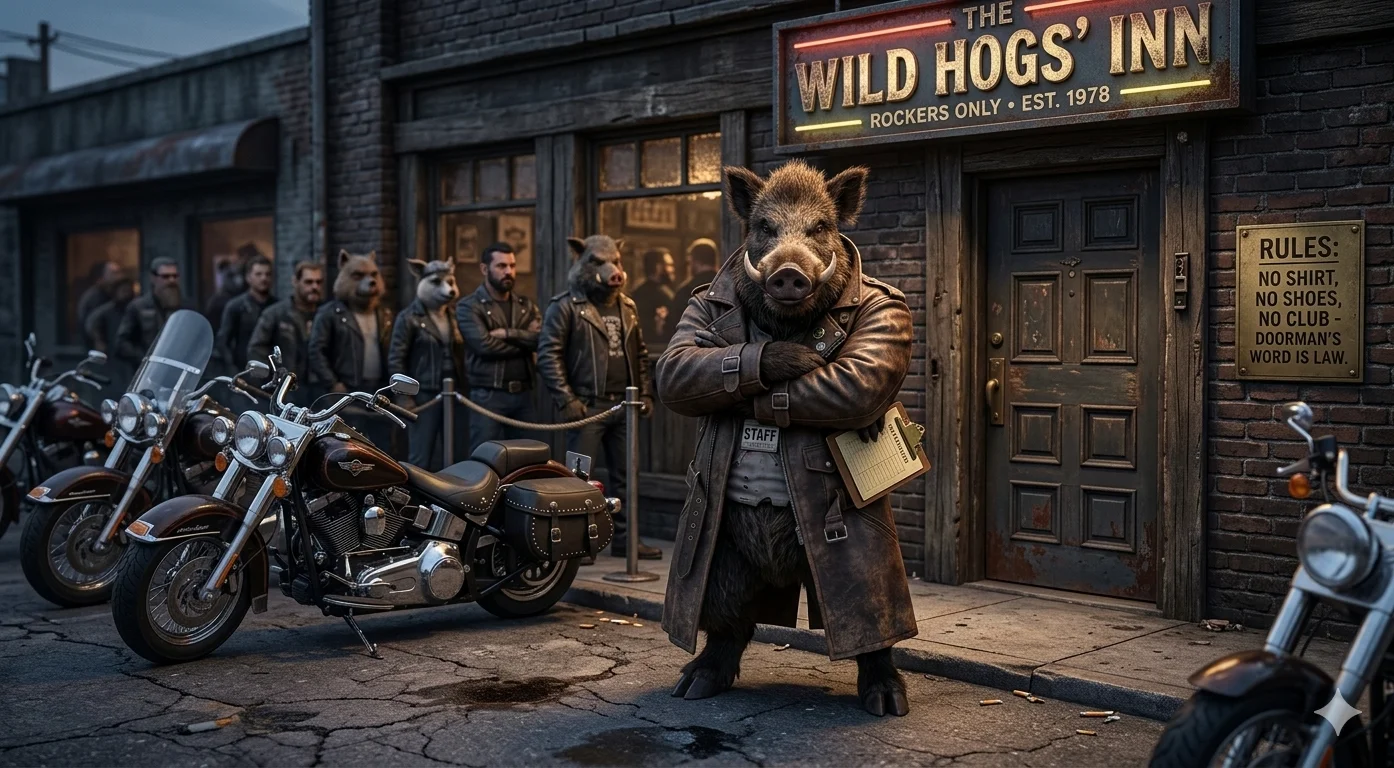
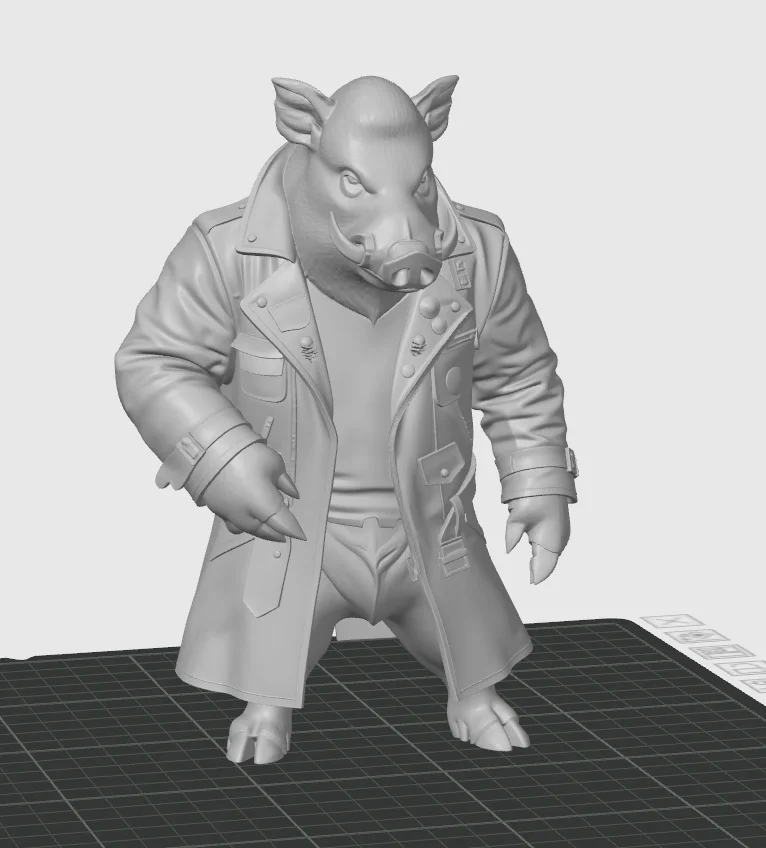
Wild Boar #5 - WildRock Animals
Dieses coole 3D-Druck-Modell ist der absolute Hingucker. Perfekt als Deco, Geschenk oder Sammlerstück!
✅ Inklusive separater Basis/Plattform – einfach danach draufkleben
Dateien enthalten:
• 1x Wild Boar 7/ Wildschwein
• 1x runde Stein-Basis
Optimierte Einstellungen für Anycubic Kobra S1 + PETG (funktioniert aber auf jedem Drucker):
Support
• Tree (auto) | Threshold 30° | First layer 90 % | Top Z 0,18 mm | Bottom Z 0,20 mm
• On build plate only + Remove small overhangs
Infill
• 10 % Gyroid | Internal solid Rectilinear | Overlap 15 %
Ironing (für mega glatte Oberflächen!)
• All top surfaces | Rectilinear | 30 mm/s | 10 % Flow
Druck-Tipps
• Nozzle 235–245 °C | Bett 70–80 °C
• Kein Raft nötig
• Tree-Supports lassen sich easy abziehen
Technische Infos
• Maßstab 1:1 (ca. 15–18 cm hoch – passt super auf den Schreibtisch)
• Getestet & druckfertig
• Hochauflösendes STL (keine Löcher, perfekte Überhänge)
Lizenz: Persönliche Nutzung erlaubt. Commercial License auf Anfrage möglich.
Danke, dass du meinen Shop unterstützt! Als Neuling freue ich mich riesig über jeden Kauf und jede Bewertung ❤
3D-Druckeinstellungen
3D-Druckeinstellungen
Druckanleitung –STL
Optimale Einstellungen für Anycubic Kobra S1 + PETG
Drucker: Anycubic Kobra S1 (0,4 mm Düse)
Filament: PETG (z. B. Anycubic PETG)
Profil: 0,20 mm High Quality @AC KS1 (nur die folgenden Änderungen!)
1. Support (wichtig für deine Überhänge)
Support aktivieren: Ja
Typ: Tree (auto)
Style: Default (Grid)
Threshold angle: 30°
First layer density: 90 %
First layer expansion: 5 mm
On build plate only: Ja
Remove small overhangs: Ja
Top Z distance: 0,18 mm
Bottom Z distance: 0,20 mm
Raft: 0 Layer (kein Raft)
Infill / Strength
Sparse infill density: 10 %
Sparse infill pattern: Gyroid
Internal solid infill pattern: Rectilinear
Infill/wall overlap: 15 %
Ironing / Oberflächenqualität
Ironing type: All top surfaces
Ironing Pattern: Rectilinear
Ironing speed: 30 mm/s
Ironing flow: 10 %
Ironing line spacing: 0,15 mm
Druck-Tipps für beste Ergebnisse
Bett auf 70–80 °C, Nozzle 235–245 °C (PETG)
Druckgeschwindigkeit: Standard (keine Speed-Profile)
Nach dem Druck Support einfach abziehen – Tree-Supports lassen sich super entfernen
Kein Raft nötig → spart Zeit und Material
Fertig!
Mit diesen Einstellungen bekommst du eine saubere, stabile und glatte Oberfläche – genau wie in meiner Vorschau.
Viel Spaß beim Drucken!
ByYvaneke589_274368Likes0Downloads5

 Bymargrave_1658465Likes0Downloads4

 ByPeterG_3243357Likes419Downloads2.2K

 ByMamuss_1991990Likes2Downloads7

 ByPapalPotato_144364Likes0Downloads7

 ByClayRadeLikes84Downloads423

 By3DPrints4meLikes0Downloads6

 BymoebisLikes0Downloads5

 Byginkel3dLikes0Downloads275

 ByabbymathLikes214Downloads2.1K

 ByStigernLikes4Downloads16

 ByRaisinCosplay_433034Likes260Downloads957