


Kẹp giữ sợi Filament
 Bytinx_1344834Likes1.2KDownloads6K
Build another version of this model.
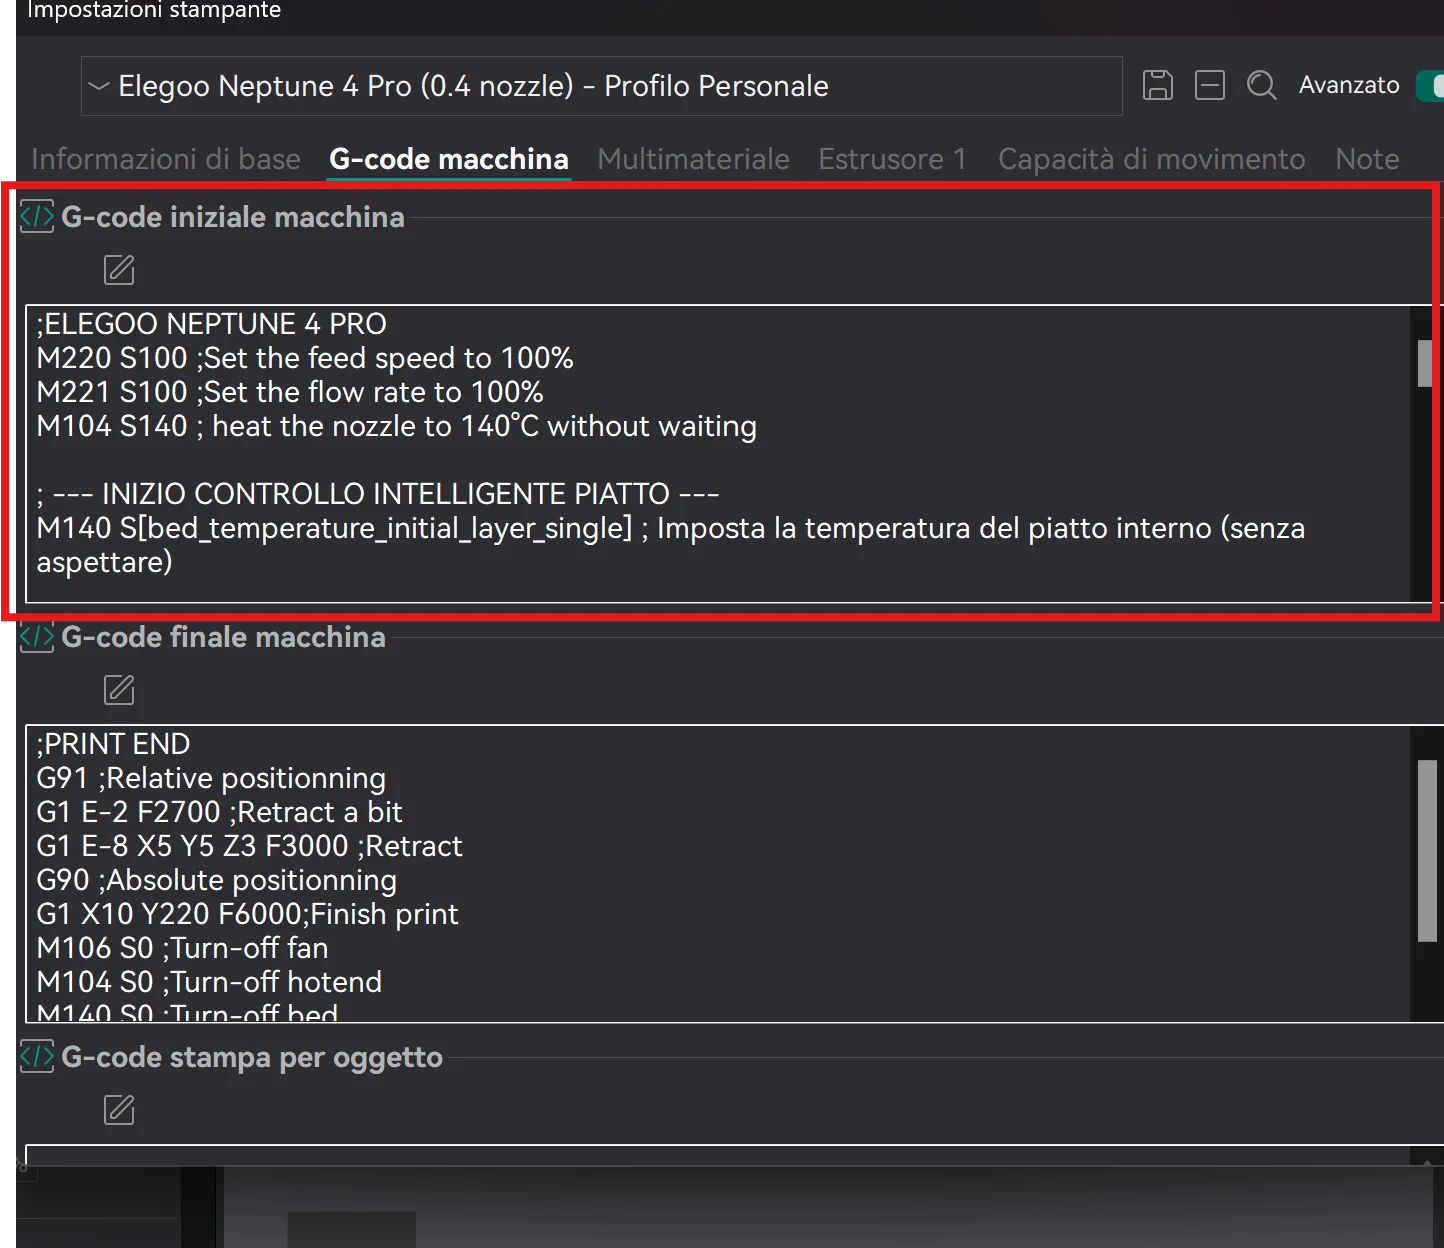
Enter the code in the section dedicated to the machine's initial g-code
;ELEGOO NEPTUNE 4 PRO
M220 S100 ;Set the feed speed to 100%
M221 S100 ;Set the flow rate to 100%
M104 S140 ; heat the nozzle to 140°C without waiting
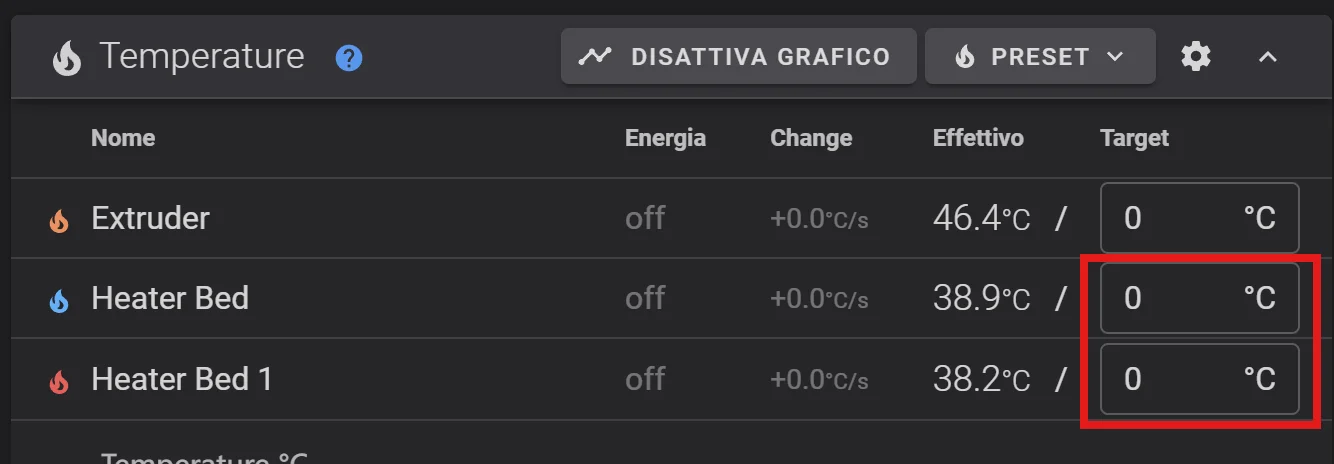
M140 S[bed_temperature_initial_layer_single]
{if first_layer_print_min[0] >= 62.5 && first_layer_print_max[0] <= 162.5 && first_layer_print_min[1] >= 62.5 && first_layer_print_max[1] <= 162.5}
M141 S0
{else}
M141 S[bed_temperature_initial_layer_single]
{endif}
TEMPERATURE_WAIT SENSOR=heater_bed MINIMUM=[bed_temperature_initial_layer_single]
G90 ; absolute positioning
G28 ;home
; Always pass ADAPTIVE_MARGIN=0 because Orca has already handled adaptive_bed_mesh_margin internally
; Make sure to set ADAPTIVE to 0 otherwise Klipper will use it's own adaptive bed mesh logic
BED_MESH_CALIBRATE mesh_min={adaptive_bed_mesh_min[0]},{adaptive_bed_mesh_min[1]} mesh_max={adaptive_bed_mesh_max[0]},{adaptive_bed_mesh_max[1]} ALGORITHM=[bed_mesh_algo] PROBE_COUNT={bed_mesh_probe_count[0]},{bed_mesh_probe_count[1]} ADAPTIVE=0 ADAPTIVE_MARGIN=0
G1 Z10 F300 ; raise the Z-axis by 10 mm at a speed of 300 mm/min
G1 X67.5 Y0 F6000
G1 Z0 F300
M109 S[nozzle_temperature_initial_layer]
G92 E0 ;Reset Extruder
G1 X67.5 Y0 Z0.4 F300 ;Move to start position
G1 X167.5 E30 F400 ;Draw the first line
G1 Z0.6 F120.0 ;Move to side a little
G1 X162.5 F3000
G92 E0 ;Reset Extruder
Bytinx_1344834Likes1.2KDownloads6K

 Byprusa-researchLikes0Downloads2.7K

 Byarhi_585078Likes64Downloads542

 Bygafyx3dLikes0Downloads121

 ByHanzo3dLikes155Downloads415

 BydarienLikes0Downloads1K

 ByGeek5DLikes147Downloads485

 ByBrokentooth_designsLikes23Downloads408

 BylaserbaconLikes0Downloads172

 ByswimLikes0Downloads109

 Byla-cave-au-chatLikes0Downloads967

 Bycrawler-3903250Likes0Downloads907