


Kẹp giữ sợi Filament
 Bytinx_1344834Likes1.2KDownloads6K
Build another version of this model.
Preheat the nozzle to 175 degrees right from the start, not just at the end
Tested with firmware versions 6.4.0 and 6.2.6
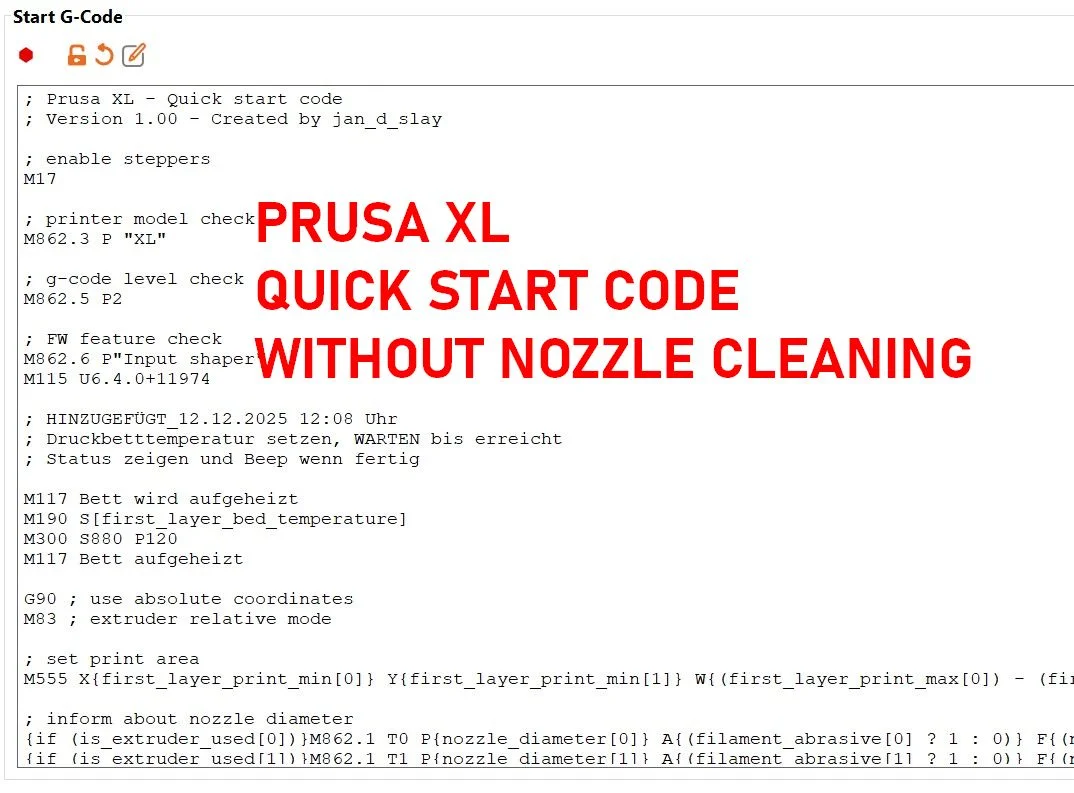
Start G-Code V1.01 modified, tested and uploaded
Bring the bed temperature to the set temperature immediately and as a first step for the first layer (blocking).
Absorb Heat disabled
Nozzle cleaning removed
Start G-Code V1.00 modified, tested and uploaded
Note on mechanical nozzle pre-cleaning added
Firmware updated to version 6.4.0
Difficulties identified before printing began
Temperature logic of the nozzle not understandable after firmware update
I am not liable for any damage caused by the use of the G-code. The G-code has been shortened in some places and the order has been changed. From my side, I can confirm that it works flawlessly on a Prusa XL with 2 toolheads.
The start GCode was copied from PrusaSlicer 2.9.4 and modified to enable smooth operation with the Prusa XL.
The nozzle MUST always be cleaned before each print. There must be NO filament residue visible on the nozzle. If this step is not followed, the print bed levelling will not work.
Before anything is moved, the print bed is set to the temperature that was set in the slicer for the first layer. The nozzle is not heated. This first command should prepare the print bed for levelling.
The print bed is at operating temperature and the nozzle is cold. With this combination, the Z-axis is ‘homed’.
No filament comes out of the mechanically cleaned nozzle. Therefore, nozzle cleaning has been completely removed from the G-code.
Bed levelling is carried out as usual. The nozzle is and remains cold.
Once bed levelling has been successfully completed, the tool head is parked. Only now is the nozzle heated to the temperature required for the first layer.
Bytinx_1344834Likes1.2KDownloads6K

 By3DSourcererLikes48Downloads377

 Byprusa-researchLikes0Downloads2.7K

 Bypeter-van-der-waalLikes0Downloads253

 ByBrokentooth_designsLikes17Downloads146

 Byarhi_585078Likes64Downloads540

 ByHanzo3dLikes155Downloads413

 BykingnothingLikes0Downloads178

 ByPengLordLikes32Downloads111

 ByPrintStructorLikes0Downloads131

 Byp3rr1ff3ryLikes0Downloads147

 BydarienLikes0Downloads1K