F3D
Kiểm Tra Flow Nâng Cao - Kalibrierung des Flusses 11 / 2

2 images

Ý Tưởng Khác

Kiểm Tra Flow Nâng Cao - Kalibrierung des Flusses

By CLPerformance

Downloads
5,662
Likes
148
Views
12,980

Files 5 371.5 KB

  • Flow_check_5mm_objekt_1765449534.stlSTL · 74.3 KB
  • Flow_check_4mm_objekt_1765449544.stlSTL · 74.3 KB
  • Flow_check_3mm_objekt_1765449547.stlSTL · 74.3 KB
  • Flow_Test_10mm_1765449556.stlSTL · 74.3 KB

Make a variant with AI

Build another version of this model.

Open Studio

Description

English below!

Eine fortschrittliche Methode zur Überprüfung der Durchflussgenauigkeit

Hinweis: Es ist absolut richtig, dass die STL aus 2 Teilen besteht! Bitte einfach den Anweisungen folgen.

die Kurzanleitung zu dieser Vorgehensweise findest Du in diesem Video:

Wie du den Flow kalibrierst:

Step 1:

  • aktiviere den Support
  • Linienstärke = Düsendurchmesser
  • Wandstärke: 0 (dies deaktiviert die variable Linienbreite)
  • Anzahl der Wandlinien: 1
  • Füllung: 100%

Step 2:

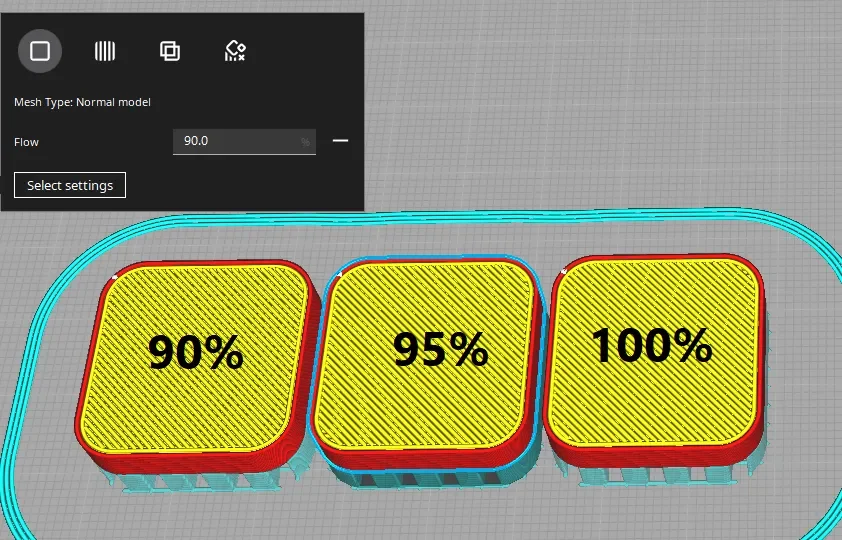
  • Füge 2 weitere Teile zu deiner Bauplatte hinzu
  • aktiviere "pro Modell Einstellung"
  • wähle "Durchfluss" als Variable
  • wähle für das 1. Modell 90%, für das zweite Modell 95%, und 100% für das letzte als Referenz

Beurteile nach dem Druck die oberste Schicht:

  • Wenn Lücken zwischen den Linien auf der obersten Hautschicht sind, ist der Fluss zu gering.
  • Wenn die Oberfläche rau ist, ist der Flow zu viel.
  • Wenn die Oberfläche schön glatt ist, ist der richtige Fluss für das aktuelle Material gefunden.

Cura Settings:

Wenn du mir eine kleine Spende zukommen lassen möchtest, dann kannst du das hier gerne tun, ohne einen Account zu erstellen: An CL Performance Spenden

English:

An Advanced way to check the flow accuracy

Note: it is absolutely correct, that both parts of this test has no connection! Please follow the instructions.

How to dail in your flow:

1st:

  • enable Supports
  • Linewidth = Nozzle diameter
  • Wall Thickness 0 (this disables the variable line width)
  • Wall Line Count: 1
  • Infill: 100%

2nd:

  • Add 2 more parts to your build plate
  • activate “per model setting”
  • choose “flow” as your variable
  • for the first test, choose 90% for the 1st model, 95% for the 2nd and 100% for the last as reference

After printing judge the top-layer:

  • if you have gaps between the lines at the top skin layer, your flow is too low
  • if the surface is rough, your flow is too high
  • if your skin is nice ans smooth, you found the correct flow for your material

This is a remix of CNC Kitchen's Extrusion test modle which can be found on thingiverse.

Read more Show less

Print spec

Formats
stl
Model files
5
Total size
371.5 KB
Largest file
74.3 KB

0 comments

See all