


Thằn lằn cử động linh hoạt - In tại chỗ (Không cần support)
 Bycream110_291842Likes924Downloads7.7K
Build another version of this model.
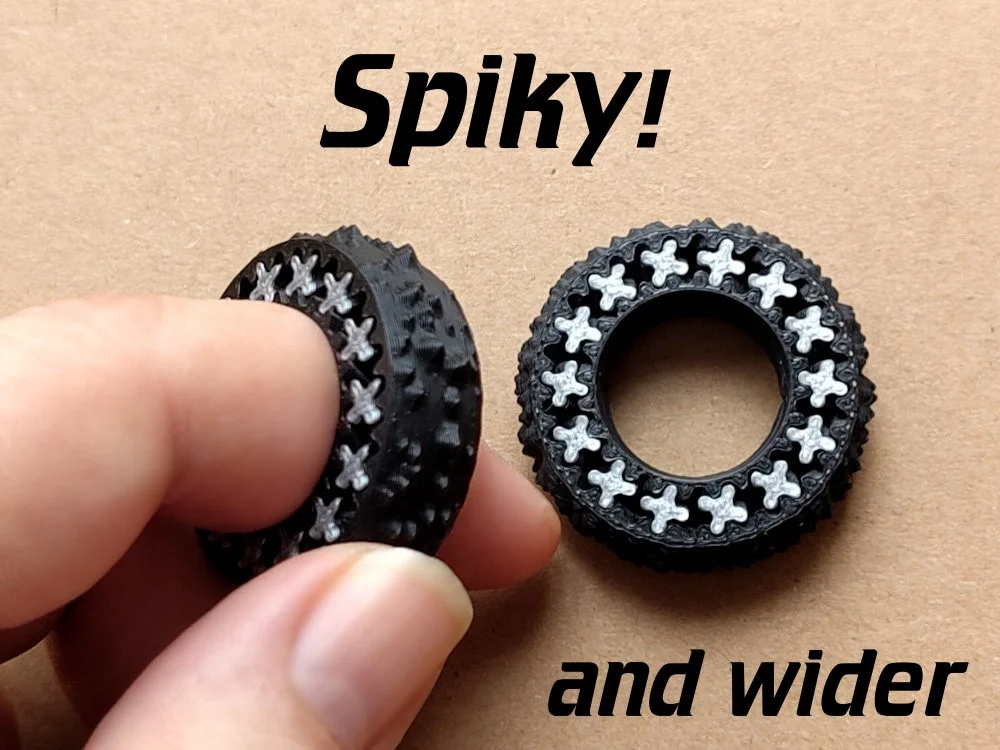
I recently got a request for a new fidget gear ring design:
And this is the result :)
Other fidget gear rings are available here.
Other spiky stim toys are available here.
--------------------------------------------------
Printing:
The 3mf files are split into 5 parts for multi-color printing.
If you choose a different color for only parts 3 and 4, only 4 color changes are required, resulting in low filament waste with single-nozzle multi-color printers. Color changes can also be done manually.
General settings:
This model requires a well dialed-in printer and filament combination; depending on these and the settings, the gears may
If you have problems with fused gears:
You can upport me on ko-fi
Have fun!
Bycream110_291842Likes924Downloads7.7K

 ByOnemoredaveLikes861Downloads6.9K

 ByCreative3D_1724906Likes66Downloads346

 ByTheMakerStuffLikes315Downloads1.9K

 BySzvmkn_3779340Likes231Downloads1.3K

 ByHacker Man ManLikes248Downloads1.5K

 Byquibeck_3353173Likes103Downloads944

 Byfluffytails37Likes184Downloads763

 Byjs14581_2767550Likes118Downloads3.3K

 ByAristotelisNellasLikes18Downloads700

 ByNoNameIdea_4437934Likes124Downloads689

 BystinovlasLikes125Downloads469